
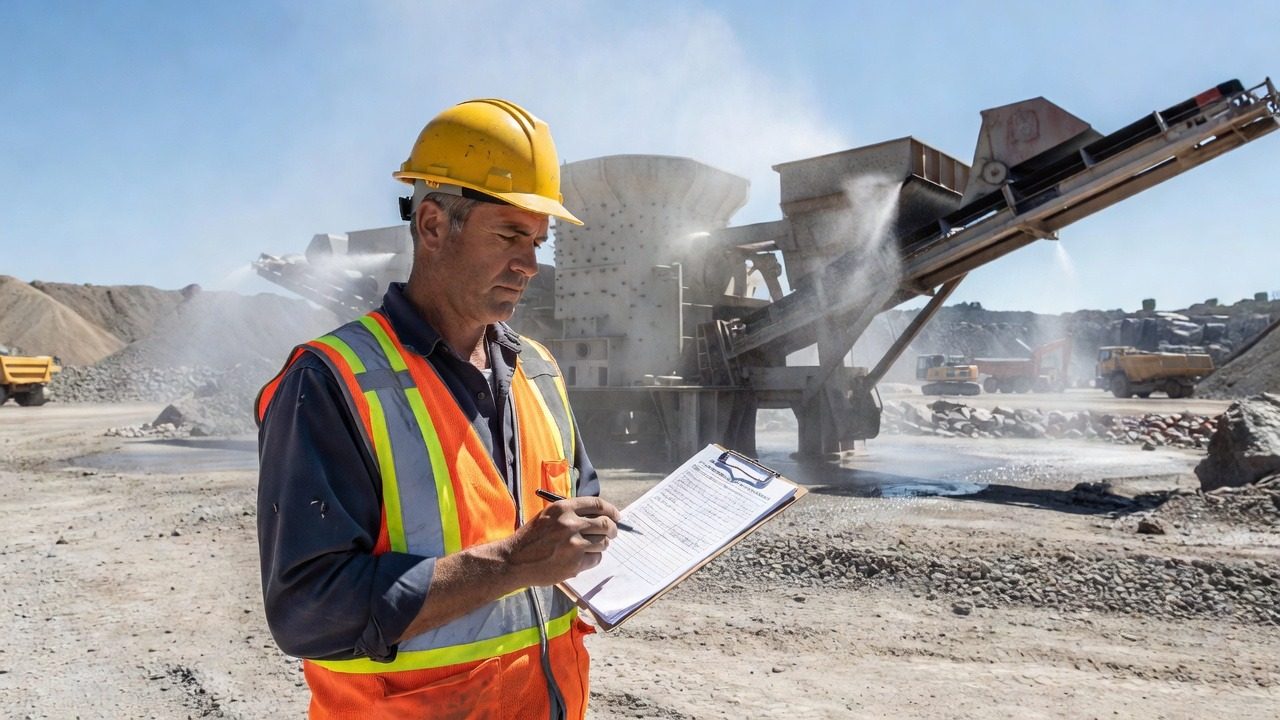
Quarry operations in the United States are under increasing scrutiny from federal and state regulators, neighboring communities, and internal safety officers. The pressure is not new, but the enforcement climate has shifted. Dust violations that were once addressed with a warning are now resulting in formal citations, operational halts, and financial penalties. For site managers overseeing active extraction and processing operations, dust management has moved from a peripheral concern to a core operational responsibility.
The challenge is not always awareness. Most experienced quarry managers understand that dust is a problem. The challenge is consistency — maintaining effective dust suppression across varying weather conditions, shifting production volumes, and multiple exposure zones simultaneously. A site that manages dust well during routine operations may still fail during peak crushing cycles, high-wind periods, or when maintenance schedules slip. What separates compliant, efficient operations from reactive ones is usually the presence of a structured, repeatable system rather than ad hoc responses to visible dust events.
This checklist is designed to give site managers a practical framework they can apply across zones, seasons, and operational shifts. It covers the categories that matter most and explains why each one carries real operational weight.
Understanding the Regulatory and Operational Stakes of Quarry Dust Control
Quarry dust control is not solely a compliance exercise — it is an operational discipline that affects worker health, equipment longevity, community relations, and a site’s ability to maintain its operating permits. When dust suppression fails, the consequences are layered. Regulatory exposure comes first, but downstream effects include increased equipment wear from airborne particulate, lost productivity when operations must pause, and reputational damage in communities where quarry expansion or renewal of use permits may be on the table.
For site managers who want a detailed operational reference to build or audit their current program, a structured Quarry Dust Control guide can help frame the right questions across each zone of a working site. The value of such a resource is not just in its recommendations, but in prompting site managers to evaluate where their current approach has gaps.
Federal standards governing respirable crystalline silica — particularly those published by OSHA and the Mine Safety and Health Administration (MSHA) — have tightened the permissible exposure limits for workers in mining and quarrying environments. The Mine Safety and Health Administration continues to prioritize silica dust enforcement in surface mining operations, and site managers should treat those standards as a floor, not a ceiling. Regulatory standards evolve, and sites that build systems aligned with best practice are better positioned to absorb future changes without significant disruption.
Why Compliance Alone Is Not Enough
Regulatory compliance sets a minimum threshold, but it does not account for the full range of operational risk that dust creates. Sites that design their dust suppression programs around the minimum required often find themselves reacting to problems that exceed what the monitoring threshold was designed to catch. Worker exposure happens across shifts and in areas that are difficult to monitor continuously. Equipment failure from dust accumulation occurs gradually, making it easy to underestimate the cost until a major repair is needed. Community complaints often precede regulatory notices, and managing public perception of a quarry’s dust output is its own form of operational risk, especially for sites operating near residential zones or in areas with active planning disputes.
Site Zoning and Source Identification
Effective dust management begins with a clear understanding of where dust is generated and in what quantities. A quarry site is not a single dust source — it is a collection of distinct zones, each with different generation rates, material types, and control requirements. Treating the entire site as a uniform problem leads to over-investment in low-risk areas and under-investment in high-risk ones.
Common dust-generating zones on a typical quarry site include the primary crushing station, secondary and tertiary processing areas, haul roads connecting the extraction face to processing, stockpile areas, transfer points on conveyors, and the site entrance and exit points where vehicles carry out dust on their tires and undercarriages. Each of these zones requires a separate assessment and a separate control approach, because the nature of the dust, the wind exposure, and the human activity patterns differ significantly between them.
Mapping Dust Sources Before Selecting Controls
Before committing to any suppression method, a site manager should conduct a systematic assessment of each zone at different times of day, during different weather conditions, and at different production volumes. A dust source that is manageable during low-output periods may become a significant problem during peak production. The mapping process should also account for wind direction patterns across the site, because a dust source that is relatively contained under calm conditions may become a widespread problem when prevailing winds carry particulate toward worker areas or site boundaries.
This mapping exercise does not need to be a formal engineering study, but it should result in a documented zone-by-zone inventory that site managers and supervisors can reference when planning suppression activities or investigating complaints.
Haul Road Dust Suppression
Haul roads are among the most persistent and difficult dust sources on any quarry site. Vehicle traffic on unpaved surfaces generates continuous particulate lift, and the problem intensifies as road surfaces dry out, break down under repeated heavy loads, or are not treated consistently. Unlike fixed processing equipment, haul roads are dynamic — their condition changes daily based on traffic volume, temperature, and moisture levels.
Water application is the most commonly used treatment for haul roads, but water alone is rarely sufficient in dry or warm climates. It evaporates quickly, requiring repeated application throughout the day, and on heavily trafficked routes, the intervals between effective wet periods can be short enough that dust control breaks down during busy operational windows. This creates a gap between the appearance of dust management activity and the actual suppression of airborne particulate.
Choosing Suppression Methods That Match Road Conditions
The selection of a haul road suppression method should be driven by the road’s traffic intensity, the material composition of the road surface, the climate conditions at the site, and the available application infrastructure. Chemical dust suppressants — which include hygroscopic salts, polymer emulsions, and other binders — are used on many heavy-traffic haul roads because they provide extended suppression between applications and reduce the total volume of water needed. However, the effectiveness of any chemical treatment depends on surface preparation, proper application rates, and compatibility with the road base material.
Sites that rely on a single approach without periodically evaluating its effectiveness tend to accumulate maintenance debt. A treatment that worked well during a wet spring may be inadequate by midsummer, and without a scheduled review process, suppression failures may not be identified until they are already affecting air quality readings or generating complaints.
Crusher and Processing Area Controls
Processing zones — particularly primary and secondary crushers — generate high concentrations of fine particulate from the mechanical breakdown of rock. These areas combine the physical generation of dust with confined spaces, worker proximity, and in some cases, silica-bearing rock types that create additional health exposure risk. The combination of these factors makes crusher areas a priority zone in any dust suppression checklist.
Wet suppression systems applied directly at the crusher feed point and at transfer points are the most widely used approach. Enclosures and partial hoods reduce the spread of dust while wet systems knock down airborne particulate before it can migrate into surrounding areas. In processing areas that handle silica-bearing rock, misting systems designed to suppress at the point of generation — rather than downstream — are more effective than those applied after dust has already become airborne.
Maintenance Schedules for Suppression Equipment
Suppression systems installed at processing points are only effective when they are functioning as designed. Clogged nozzles, worn pump components, broken spray headers, and disconnected water lines are common causes of suppression failure in processing areas — and because these failures are not always visually obvious, they can go undetected during busy shifts. A suppression system that is partially functioning creates a false sense of control that can be more problematic than acknowledged equipment downtime, because managers and workers may assume dust exposure is being managed when it is not.
Maintenance checks for suppression equipment should be integrated into shift startup routines, not treated as standalone maintenance tasks. The person responsible for confirming that suppression systems are active and functioning should be identified by name on each shift, and a simple verification log — covering flow confirmation, nozzle inspection, and system pressure — provides the documentation that regulators may request during site inspections.
Stockpile and Transfer Point Management
Stockpiles and conveyor transfer points generate dust differently than active processing zones. Stockpiles generate dust during loading, unloading, and when exposed to wind — particularly when stockpiled material has dried out or when wind speeds are elevated. Transfer points on conveyors produce dust from the impact of material falling between belt sections, and the fine fraction of the material becomes airborne at these points regardless of the overall moisture content of the bulk load.
Management of these areas often receives less attention than crusher stations because the dust events appear less dramatic during routine observation. However, transfer points and stockpile boundaries are common sources of boundary exceedances and community-visible dust plumes, particularly in dry conditions or when wind direction puts them in line with the site perimeter.
Wind as an Unmanaged Variable
Most dust suppression planning addresses dust generation but underestimates the role of wind in converting a localized dust source into a site-wide or off-site problem. Wind speed and direction affect how much suppression is needed at any given time, but most fixed suppression systems are not responsive to wind conditions — they operate on a fixed schedule or continuous flow regardless of ambient conditions. Sites that integrate basic weather monitoring into their dust management decision-making are better positioned to adjust suppression intensity before visible dust events develop, rather than responding after the fact.
Record-Keeping, Reporting, and Internal Auditing
A dust suppression program without documentation is difficult to defend during a regulatory review and nearly impossible to improve over time. Record-keeping serves two purposes: it demonstrates good-faith compliance efforts to regulators, and it creates the data that allows site managers to identify which control measures are performing and which need adjustment.
Records that support a strong dust management program include inspection logs for suppression equipment, water application records for haul roads, maintenance logs for processing area systems, incident documentation for visible dust events or complaints, and training records for workers operating suppression equipment. These records do not need to be complex, but they do need to be consistent, accurately dated, and stored in a way that is accessible to site management and retrievable during inspections.
Internal Auditing as a Continuous Improvement Tool
A quarterly internal audit of the dust suppression program — reviewed by a site manager who was not responsible for day-to-day implementation during that period — provides the independent perspective that self-assessment often lacks. The audit should evaluate whether control measures were applied as planned, whether equipment was maintained on schedule, whether any dust complaints or incidents occurred and how they were addressed, and whether the program’s zone-by-zone assessments remain current given any changes in production volume or site layout.
Conclusion
Quarry dust control is most effective when it is treated as a managed system rather than a reactive response to visible problems. The sites that perform well under regulatory scrutiny and maintain productive relationships with surrounding communities are generally those where dust suppression is embedded into daily operations — not bolted on as an afterthought when a complaint arrives or an inspection is scheduled.
The checklist framework outlined here is not exhaustive, but it covers the categories that most commonly determine whether a site’s dust program is sustainable or fragile. Zone identification, method selection matched to actual conditions, equipment maintenance integrated into shift routines, wind awareness, and consistent documentation are the structural elements that determine real-world performance. Sites that address these categories deliberately, and revisit them regularly as conditions change, are far better positioned to manage both the regulatory and operational dimensions of dust control through 2025 and beyond.
