
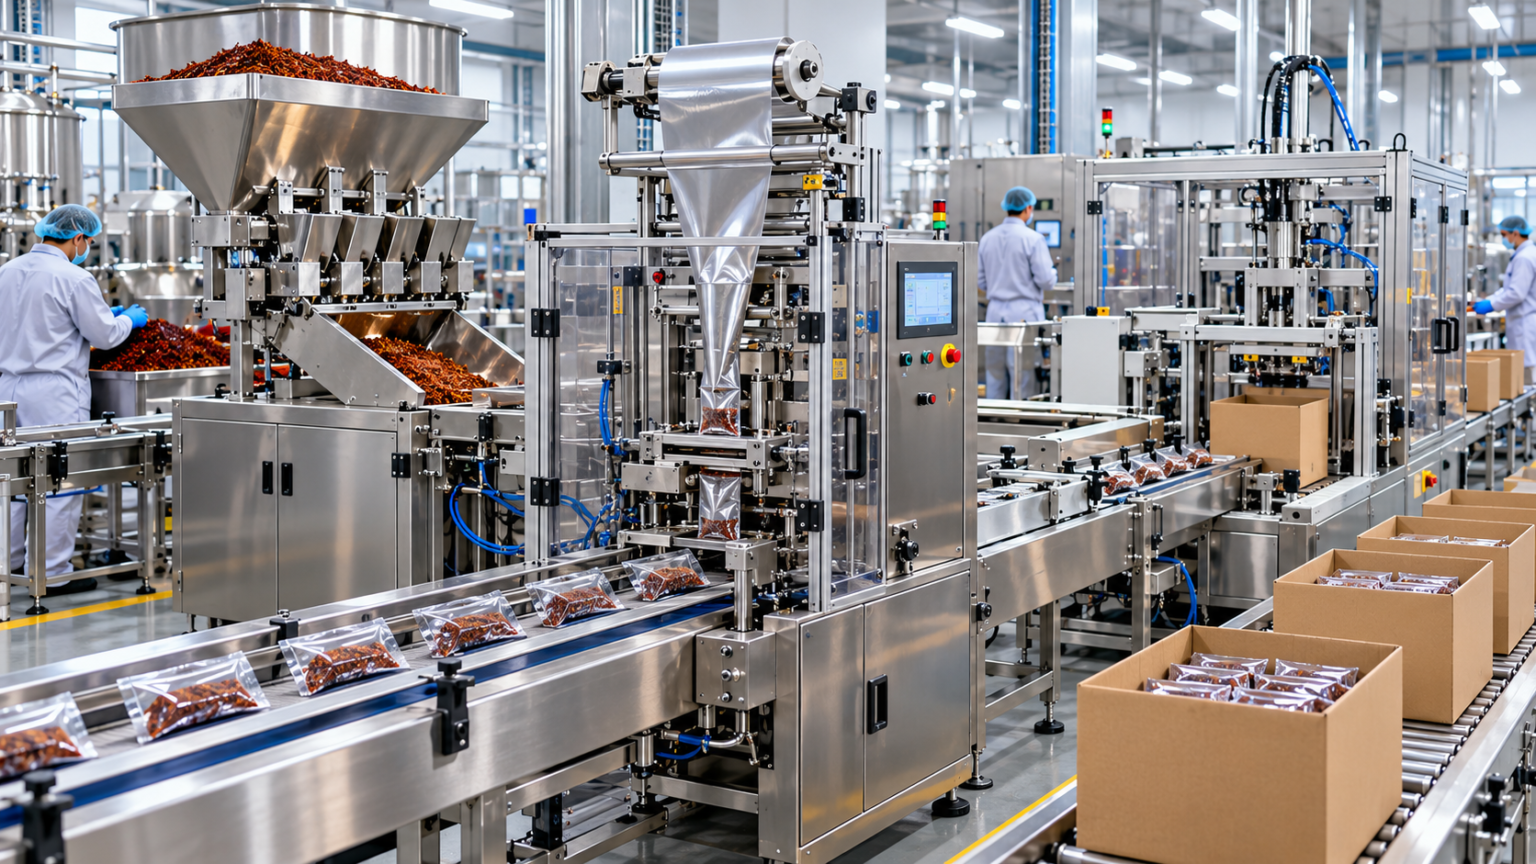
Industrial packaging requires consistent product measurement, controlled material handling, dependable sealing, and effective quality management. These requirements become particularly important when manufacturers operate high-speed production lines with multiple connected machines. The 100-120 PPM Shisha Tobacco Packaging Line is an example of an integrated industrial system designed to measure, fill, seal, and pack processed waterpipe tobacco into finished packages through coordinated mechanical and electronic operations.
Unlike many dry granular materials, molasses-based shisha tobacco has a distinctive physical consistency. The combination of tobacco, moisture, sweeteners, and flavouring ingredients can produce a sticky, cohesive material that requires specialised handling equipment.
This creates challenges involving feeding, portion measurement, residue accumulation, packaging compatibility, and cleaning.
A packaging system must accommodate these material characteristics while maintaining suitable operational controls.
Modern automation can help coordinate several production stages within one integrated process, although actual performance depends on equipment configuration, material consistency, maintenance, and operating conditions.
For industrial engineers and equipment procurement professionals, understanding the machinery’s capabilities and limitations is essential.
This guide examines seven technical considerations associated with high-speed shisha tobacco packaging, alongside equipment specifications, safety requirements, regulatory responsibilities, and maintenance practices.
What Is a 100-120 PPM Shisha Tobacco Packaging Line?
A 100-120 PPM shisha tobacco packaging line is a coordinated industrial system intended to process and package measured quantities of prepared waterpipe tobacco.
In this context, PPM means packages per minute.
A nominal speed of 100–120 PPM describes a production rate of approximately 100 to 120 finished packages per minute under specified operating conditions.
Such systems may combine material feeding, portion measurement, filling, sealing, cartoning, and product transfer equipment.
The exact machinery included depends on the manufacturer’s design and the purchased configuration.
How an Integrated Packaging Line Works
An automated packaging process begins with prepared material entering a controlled feeding arrangement.
The equipment transfers material towards a portion-measuring station.
A dosing or weighing system determines the intended amount before it is placed into suitable packaging.
The package then moves through the appropriate sealing equipment.
Additional machinery may transfer the sealed product into cartons, apply required markings, and prepare the units for secondary packaging.
Sensors, controllers, conveyors, and mechanical drives coordinate these operations.
Why Shisha Tobacco Requires Specialised Handling
Waterpipe tobacco mixtures often contain ingredients that influence their physical flow characteristics.
The material may adhere to surfaces, form clumps, or resist free movement through conventional dry-material feeding equipment.
Changes in consistency between batches may affect portion measurement.
The equipment must therefore be evaluated using representative material samples.
The term high-speed does not mean that every formulation can be handled at the same production rate.
1. Automated Equipment Supports Consistent Production Throughput
One important characteristic of integrated packaging equipment is the ability to coordinate multiple mechanical operations within a repeatable sequence.
In manually operated facilities, separate handling and packaging stages may require frequent employee intervention.
An automated line instead uses machinery to manage the movement of material between stations.
Understanding the Rated Production Speed
The JCS-120 packaging line is advertised with an operating speed of 100–120 packages per minute.
At the upper and lower stated rates, the theoretical output ranges from 6,000 to 7,200 packages during an uninterrupted hour.
This represents nominal machine capacity rather than guaranteed production output.
Actual throughput is affected by material feeding, packaging supply, equipment adjustments, inspection requirements, and unplanned stoppages.
Coordinating Connected Machines
A complete packaging system contains several interdependent operations.
If a filling unit runs faster than the sealing station, unfinished products may accumulate.
Similarly, interruptions in material feeding can leave downstream equipment waiting for product.
Coordinated machinery operation helps maintain an orderly production flow.
The system should be evaluated as a complete line rather than a collection of independent machines.
Measuring Real Operating Performance
Factory managers often use overall equipment effectiveness and related measures to examine industrial productivity.
Important considerations include equipment availability, actual running speed, and the proportion of output meeting quality requirements.
A machine’s published maximum speed represents only one part of the performance assessment.
Evaluating Production Stability
Stable operation depends on consistent material feeding and reliable equipment settings.
Engineers should examine how the system responds to temporary interruptions, incomplete fills, and packaging material faults.
A well-designed production line should provide appropriate fault detection and recovery procedures.
2. Precision Weighing Helps Maintain Package Quantity Consistency
Portion measurement is a critical part of packaging equipment performance.
The quantity placed inside each package must conform to the applicable product specification and destination market’s weights and measures requirements.
Understanding Weighing Accuracy
The JCS-120 manufacturer’s published specification lists a weight accuracy of ±1.5%.
This figure describes an advertised machine characteristic.
It should not be interpreted as proof that every package will satisfy applicable net-quantity regulations without further verification.
Actual performance may vary according to material consistency and operating conditions.
Why Material Consistency Matters
Cohesive materials can be more difficult to portion consistently than free-flowing powders.
Variations in moisture, texture, and material distribution can affect feeding.
If material reaches the weighing station inconsistently, the machine may require additional adjustments or intervention.
A suitable assessment should therefore include representative samples from normal production batches.
Calibrating Weighing Equipment
Calibration helps establish a reliable relationship between the machine’s measurement system and an appropriate reference.
Equipment should be checked using suitable calibrated instruments.
The frequency of verification depends on the manufacturing quality system and relevant regulatory requirements.
A change in product characteristics may require additional assessment.
Detecting Incorrect Package Weights
Some production systems incorporate checkweighers or other inspection equipment.
These devices can identify packages outside established acceptance limits.
A checkweigher may also provide information about recurring filling variation.
The response to an underweight or overweight package should follow documented quality procedures.
Maintaining Measurement Records
Batch documentation can include target quantity, machine settings, inspection results, and corrective actions.
These records support production traceability and help engineers identify changes in equipment performance.
3. Integrated Sealing Equipment Supports Package Integrity
Packaging must retain its intended closure throughout routine handling, storage, and transportation.
The suitability of the seal depends on the selected packaging material, sealing mechanism, operating settings, and package contents.
Understanding the Sealing Process
Many flexible packaging systems use materials containing a heat-sealable layer.
The equipment applies controlled temperature, pressure, and contact time to form the closure.
Other packaging structures may require different sealing methods.
The exact configuration should be confirmed with the equipment supplier.
The Importance of Seal Area Cleanliness
Sticky materials can create particular challenges near sealing surfaces.
Product contamination in the seal area may interfere with the formation of a consistent closure.
Mechanical timing and package positioning should be designed to limit unwanted contamination.
The problem cannot always be resolved simply by increasing the sealing temperature.
Double Sealing Arrangements
Shishapack advertises a double sealing system for its JCS-120 packaging line.
A dual-sealing arrangement may be used to provide an additional sealing operation within the packaging process.
However, the term double sealing does not independently establish a particular seal-strength result or guarantee that every package will be leak-free.
The actual construction and testing requirements should be documented.
Evaluating Seal Quality
Appropriate testing may include visual inspection and defined seal-integrity procedures.
The selected method depends on package construction, product characteristics, and the quality requirements of the manufacturer.
Where moisture and aroma retention are relevant, the complete packaging structure must also be evaluated for its barrier properties.
Packaging Materials and Compatibility
Films vary in thickness, stiffness, sealant chemistry, and barrier performance.
A material that seals effectively on one machine may need different settings on another.
Suppliers should verify compatibility using production-representative trials.
4. Servo and Cam Mechanisms Provide Controlled Machine Movement
High-speed packaging involves repeated mechanical movements.
Products must be positioned, transferred, enclosed, and discharged in the correct sequence.
Motion control systems play an important role in coordinating these activities.
Understanding Servo Motors
Servo motors provide electronically controlled movement.
They can be used to manage position, speed, and acceleration in suitable industrial mechanisms.
In packaging equipment, this may help coordinate individual operations with the machine’s production cycle.
Actual performance depends on controller configuration, mechanical design, and maintenance.
The Role of Cam Mechanisms
Cam-driven mechanisms use designed mechanical profiles to produce repeated movements.
They are widely used in industrial machinery where precise and repeatable mechanical action is required.
The suitability of a cam mechanism depends on load, speed, alignment, lubrication, and other engineering considerations.
Combining Different Motion Technologies
The JCS-120 product description identifies servo and cam structures as part of the equipment.
These technologies may serve different functions within the complete packaging system.
One type of drive should not automatically be considered superior for every operation.
The important requirement is that the mechanisms perform their intended functions reliably.
Mechanical Wear and Maintenance
Moving components require appropriate inspection.
Bearings, drive elements, fasteners, guides, and other components may deteriorate over time.
A documented maintenance programme helps identify developing problems before they affect production.
Control System Compatibility
Controllers must coordinate machine movements with sensors and safety devices.
Technicians should verify that the installed system can detect faults and respond according to the approved safety design.
Production speed should never be increased by bypassing protective devices.
5. Controlled Changeovers Help Manage Different Product Batches
Manufacturing facilities may process different formulations or packaging specifications on the same equipment.
Changing between products requires careful handling to prevent unintended carryover and maintain accurate production records.
Understanding Product Changeover
A changeover may involve clearing residual material, cleaning equipment, adjusting operating parameters, and verifying the next batch.
The required procedure depends on the product and packaging arrangement.
Manufacturer-Advertised Changeover Capability
Shishapack states that the JCS-120 can support flavour changeovers in as little as ten minutes.
This is a manufacturer-published claim and should be treated as a best-case performance figure rather than a universal expectation.
The actual duration may depend on the formulation, amount of residue, cleaning requirements, and equipment configuration.
Preventing Unintended Carryover
Residual material from a previous batch can affect the composition of the next product.
Appropriate cleaning and inspection are therefore important.
Facilities should establish procedures suited to the relevant formulations and their quality requirements.
Managing Recipe Settings
Programmable equipment may allow operators to store approved machine settings.
Where available, these settings can support repeatability between batches.
However, stored settings do not eliminate the need for checks and documented approval.
Maintaining Batch Identification
Production teams should document material batches, packaging specifications, process settings, and finished product identification.
Reliable records support quality investigations and regulatory reporting where applicable.
6. Safety Systems Support Controlled Industrial Operations
Industrial packaging lines contain multiple potential hazards.
These can include conveyors, moving machine parts, sealing equipment, compressed air, and electrical systems.
Appropriate risk assessment is necessary before installation and operation.
Machine Guarding
The JCS-120 is advertised with a full-line protective cover and safety sensing arrangements.
These are relevant features, but their adequacy must be assessed against the actual machine hazards.
Protective devices should prevent access to dangerous motion where required.
Emergency Stop Arrangements
Emergency stopping equipment can help operators respond to hazardous situations.
The location and performance of emergency stop devices should follow the applicable machinery safety design.
An emergency stop is not a replacement for mechanical guarding or energy isolation.
Electrical and Pneumatic Safety
The line uses electrical power and compressed air.
Both systems require appropriate installation, inspection, and maintenance.
Stored pneumatic energy and unexpected movement may create hazards during servicing.
Applicable Safety Guidance
ISO 12100:2010 establishes general principles for machinery risk assessment and risk reduction.
In the United States, OSHA 29 CFR 1910.212 addresses machine guarding, while 29 CFR 1910.147 covers hazardous-energy control during specified servicing and maintenance activities.
The actual legal requirements depend on the installation jurisdiction.
Employee Training
Operators should understand the equipment’s intended use, controls, fault indications, and emergency procedures.
Maintenance personnel require additional instruction appropriate to their responsibilities.
No production objective should justify defeating safety interlocks.
7. Integrated Cartoning Supports Organised Secondary Packaging
The final stage of a packaging line may involve transferring finished units into cartons or other distribution packaging.
This operation requires coordination between the primary package output and the secondary packaging equipment.
Understanding Cartoning
A cartoning machine places appropriately prepared products into cartons.
Depending on its design, the machine may also erect, close, or transfer cartons.
The exact functions should be verified for the purchased equipment.
Coordinating Package and Carton Movement
The primary packaging station must supply products in a suitable arrangement for cartoning.
Conveyors, guides, and sensors help manage this transfer.
If cartons are unavailable or incorrectly positioned, the line should respond according to its approved operating logic.
Applying Required Information
Tobacco product packaging is subject to significant legal restrictions in many jurisdictions.
These can include health warnings, product identification, tax markings, and other mandatory information.
A cartoning system must accommodate the required package design without concealing or damaging legally mandated warnings.
Preparing for Distribution
Finished cartons may require additional inspection or secondary shipping protection.
The relevant packaging should be appropriate for the expected transportation conditions.
Maintaining Traceability
Batch codes, production records, and appropriate carton identification can help link shipped products to their manufacturing information.
The specific system depends on the manufacturer’s legal obligations and quality procedures.
Shishapack JCS-120: Manufacturer-Published Technical Specifications
The JCS-120 is identified by Shishapack as a complete high-speed system for packaging processed waterpipe tobacco.
Its published specification provides an initial basis for engineering evaluation.
Model: JCS-120
Advertised Speed: 100–120 packages per minute
Nominal Package Weight Range: 25–60 g
Advertised Weight Accuracy: ±1.5%
Overall Line Dimensions: Approximately 10 × 8 × 2 metres
Required Air Pressure: 0.6–0.8 MPa
Published Total Power: 25 kW
Electrical Supply: 380 V, 50 Hz
Identified Technologies: Servo and cam mechanisms, protective safety covers, and double sealing arrangements
Advertised Changeover Time: As little as ten minutes under suitable conditions
The above figures are based on the manufacturer’s product listing and should be confirmed using an up-to-date technical datasheet.
The actual equipment arrangement, output, dimensions, utilities, and safety features may depend on the configuration ordered.
Understanding the Line Footprint
The published dimensions describe an approximately ten-metre by eight-metre footprint, with a stated height of about two metres.
Factory planning should account for more than the machine’s physical dimensions.
Operators need suitable access for material supply, maintenance, inspection, and emergency evacuation.
Installation drawings should therefore include required service clearances and supporting equipment.
Evaluating Electrical Requirements
A published power rating does not establish the machine’s actual energy consumption in every operating state.
Electrical engineers should confirm the supply arrangement, motor loads, protection requirements, and installation conditions.
Evaluating Compressed Air Requirements
The advertised operating pressure range is 0.6–0.8 MPa.
Pressure is only one part of the compressed-air requirement.
The supplier should also specify air consumption, required air quality, connection details, and allowable fluctuations.
Regulatory Responsibilities for Shisha Tobacco Packaging
Tobacco packaging has additional obligations beyond ordinary industrial packaging.
Waterpipe tobacco contains nicotine and is associated with serious health risks. Packaging automation does not make the tobacco product safe or reduce the health risks of consuming it.
Health Warning Requirements
In the United States, hookah or waterpipe tobacco is covered by FDA tobacco product regulations.
Applicable products must carry required nicotine warning statements under the relevant federal labeling rules.
Other countries may require pictorial warnings, prescribed warning sizes, standardised packaging, or additional statements.
Manufacturers must identify the rules applicable to every destination market.
Product Identification and Traceability
Certain jurisdictions impose specific requirements concerning tobacco product identification, tax markings, manufacturing information, and distribution records.
The exact obligations vary significantly.
A packaging machine should be evaluated against the legally approved packaging format.
Restrictions on Promotional Claims
Packaging and related marketing materials must not make misleading claims suggesting that waterpipe tobacco is harmless or a safe alternative to other tobacco products.
The World Health Organization has published guidance supporting comprehensive regulation of waterpipe tobacco, including health warnings and restrictions on misleading representations.
Legal Review Before Production
A packaging specification should be reviewed by qualified regulatory personnel before commercial use.
Machine compatibility alone does not establish that the finished product satisfies labeling or market-entry rules.
How to Evaluate a High-Speed Packaging Line
Industrial procurement decisions should be based on documented requirements and representative performance tests.
Define the Intended Products
The evaluation should begin with information about material consistency, nominal package weight, packaging format, and required production quantities.
Changes in product properties may affect equipment performance.
Review the Complete Line Configuration
Ask which stations are included and which are optional.
The quotation should identify material feeding, weighing, primary packaging, sealing, cartoning, and any additional equipment.
A complete line description avoids misunderstandings about what is supplied.
Verify Production Capacity
The supplier should demonstrate achievable output using representative materials and approved packaging components.
The test should record stoppages, rejected packages, and other conditions affecting performance.
Confirm Quality Criteria
Define appropriate acceptance limits for net quantity, seal integrity, finished package appearance, and relevant markings.
The test procedure should specify how these characteristics will be assessed.
Examine Maintenance Accessibility
The equipment should provide appropriate access for inspection, servicing, and approved cleaning.
Review the availability of replacement components and the expected maintenance requirements.
Assess Safety Documentation
Request appropriate risk assessment information, operating instructions, electrical drawings, and details of protective systems.
The final installation should be inspected according to applicable requirements.
Review Supplier Support
Clarify installation responsibilities, training, spare parts, documentation, warranty terms, and technical assistance.
All commitments should be confirmed in writing.
Installation and Commissioning Considerations
Commissioning is the process of verifying that installed equipment performs according to the agreed specifications.
A high-speed packaging line should not begin unrestricted operation until appropriate safety and functional testing has been completed.
Preparing the Site
The factory should provide suitable floor space, equipment support, ventilation, electrical services, and compressed-air supply.
Relevant environmental and workplace safety requirements should be assessed.
Verifying Mechanical Alignment
Conveyors and connected machines should be positioned according to approved installation drawings.
Poor alignment can cause product transfer problems and unnecessary wear.
Testing Safety Functions
Guards, protective sensing systems, emergency stops, and other required safeguards must be tested.
The complete line should respond safely to foreseeable operating faults.
Checking Weighing Performance
The weighing system should be verified using suitable reference equipment.
Testing should use representative material under relevant production conditions.
Inspecting Packaging Quality
Samples should be examined for net quantity, correct closure, packaging integrity, and required markings.
Failures should be investigated before approving routine production.
Recording Commissioning Results
The commissioning record should include accepted settings, test results, corrective actions, and any unresolved limitations.
This information provides a reference for future maintenance and quality investigations.
Maintenance Requirements for High-Speed Packaging Machinery
Preventive maintenance is important for equipment with frequent moving cycles.
The appropriate schedule should follow the manufacturer’s instructions and consider actual operating hours and environmental conditions.
Inspect Mechanical Drives
Servo and cam mechanisms should be examined according to their specified maintenance requirements.
Unexpected noise, vibration, or positioning errors should be investigated.
Maintain Product Contact Areas
Residue accumulation can affect equipment performance.
Cleaning methods must be compatible with the machinery and product characteristics.
Check Weighing Accuracy
Routine verification can identify changes in measurement performance.
Any deviations should be investigated through documented procedures.
Examine Sealing Components
Sealing surfaces and associated mechanisms should be checked for wear, contamination, and alignment.
Inspect Sensors and Guards
Safety devices and operational sensors should remain functional.
Damaged or bypassed safeguards require immediate attention.
Maintain Electrical and Pneumatic Systems
Cables, connections, air lines, and related components should be inspected by qualified personnel.
Maintenance should follow appropriate energy isolation procedures.
Record Repairs and Replacements
A documented service history can help identify recurring failures and support future maintenance decisions.
Common Operational Problems and Their Causes
Even well-designed automated lines can experience performance problems.
Effective troubleshooting begins with identifying the actual cause rather than changing several settings simultaneously.
Inconsistent Portion Weights
Variation may be associated with material feeding, measurement calibration, or changing product characteristics.
The weighing and feeding processes should be evaluated together.
Unreliable Package Seals
Incorrect sealing conditions, contaminated seal surfaces, or incompatible packaging materials can contribute to closure defects.
Product Accumulation
If one production station operates more slowly than another, material or finished packages may accumulate.
The complete line should be evaluated for bottlenecks.
Frequent Sensor Faults
Misalignment, contamination, wiring problems, or component failure may affect detection.
Increased Mechanical Vibration
Vibration can indicate wear, misalignment, or other mechanical conditions.
Qualified technicians should investigate before the problem becomes severe.
Extended Changeover Time
Longer-than-expected changeovers may result from cleaning requirements, product residue, mechanical adjustments, or additional quality verification.
The published minimum changeover time should not be treated as a mandatory operating target.
Total Cost of Ownership and Procurement Planning
The financial assessment of industrial machinery should extend beyond the initial purchase price.
Equipment and Integration Costs
The system may require additional conveyors, inspection devices, utilities, or modifications to the factory.
These costs should be identified during planning.
Installation and Commissioning
International equipment purchases can involve freight, customs charges, installation, testing, and personnel training.
Operating Expenses
Electricity, compressed air, maintenance, approved cleaning materials, and packaging consumables contribute to the operating cost.
Spare Parts
Replacement components should be available through a documented supply arrangement.
Long delays in obtaining critical parts can affect production planning.
Downtime and Quality Losses
Unplanned stoppages and rejected packages have financial consequences.
The evaluation should consider realistic operating data rather than assuming continuous operation at nominal speed.
Long-Term Support
Technical documentation, training, and continued service availability are important considerations for complex equipment.
Frequently Asked Questions
1. What is a 100-120 PPM Shisha Tobacco Packaging Line?
It is an integrated industrial packaging system designed to measure, fill, seal, and pack processed waterpipe tobacco at a nominal speed of 100–120 packages per minute.
2. What are the JCS-120 machine’s published specifications?
Shishapack lists a 25–60 g package weight range, ±1.5% weighing accuracy, 25 kW power rating, 380 V electrical supply, and 0.6–0.8 MPa air pressure requirement.
3. Does the advertised 100–120 PPM speed guarantee actual factory output?
No. Actual output depends on material consistency, packaging format, maintenance, quality checks, and operating interruptions.
4. What is the purpose of the double sealing system?
The manufacturer describes a double sealing arrangement intended to support package closure. Actual integrity must be confirmed through suitable testing.
5. What safety requirements should be considered?
Machinery guarding, electrical protection, hazardous-energy isolation, operator training, and an appropriate risk assessment are important. Legal requirements depend on the installation jurisdiction.
6. Does automated shisha tobacco packaging guarantee regulatory compliance?
No. Finished tobacco packages must independently meet applicable health-warning, labeling, traceability, and other legal requirements for the intended market.
Conclusion
The 100-120 PPM Shisha Tobacco Packaging Line illustrates how multiple industrial packaging operations can be coordinated through an automated system. Its published JCS-120 specifications describe high-speed operation, controlled weighing, servo and cam mechanisms, and integrated sealing and cartoning processes. Actual performance must be verified through representative testing, appropriate machinery safeguards, and quality procedures. For regulated tobacco products, technical packaging performance must also be considered separately from mandatory health warnings, legal compliance, and the documented risks of tobacco use.
